
CDL600 Curling and Lining Machine
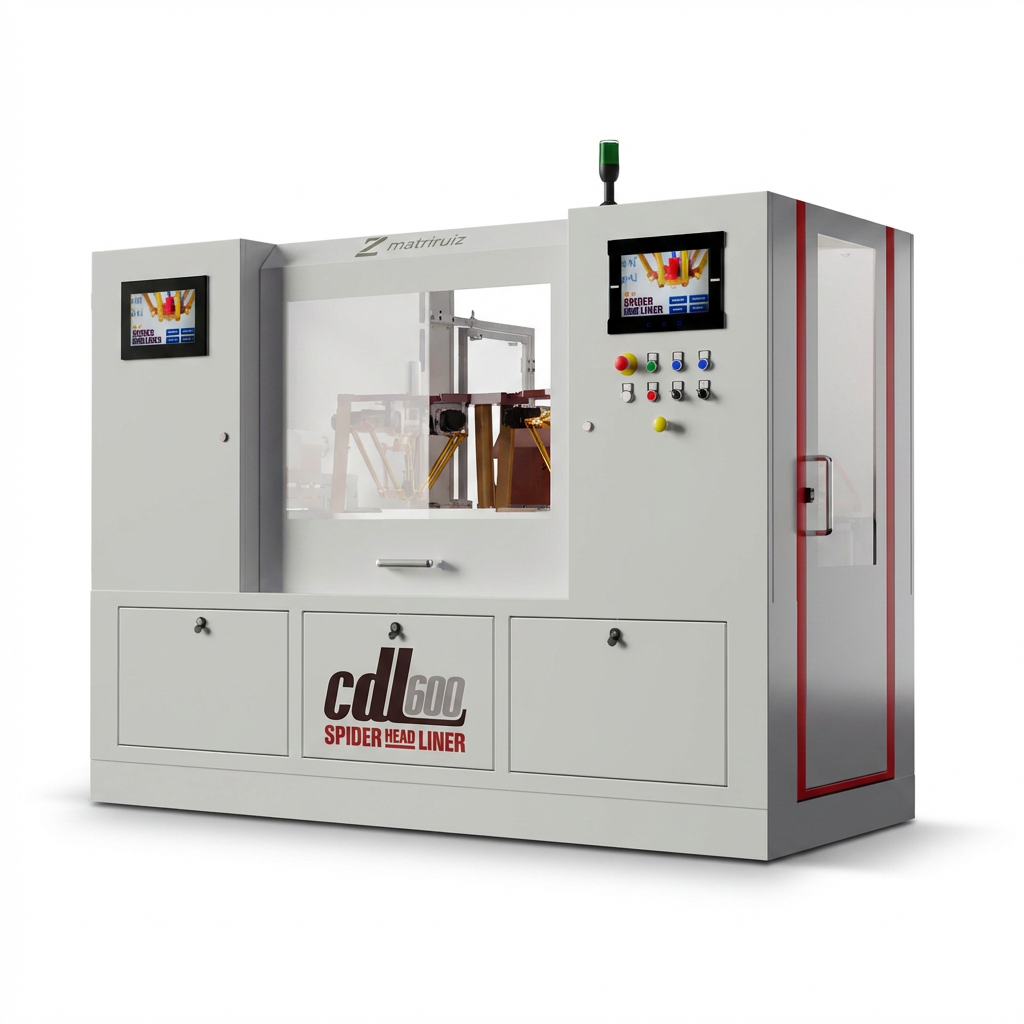
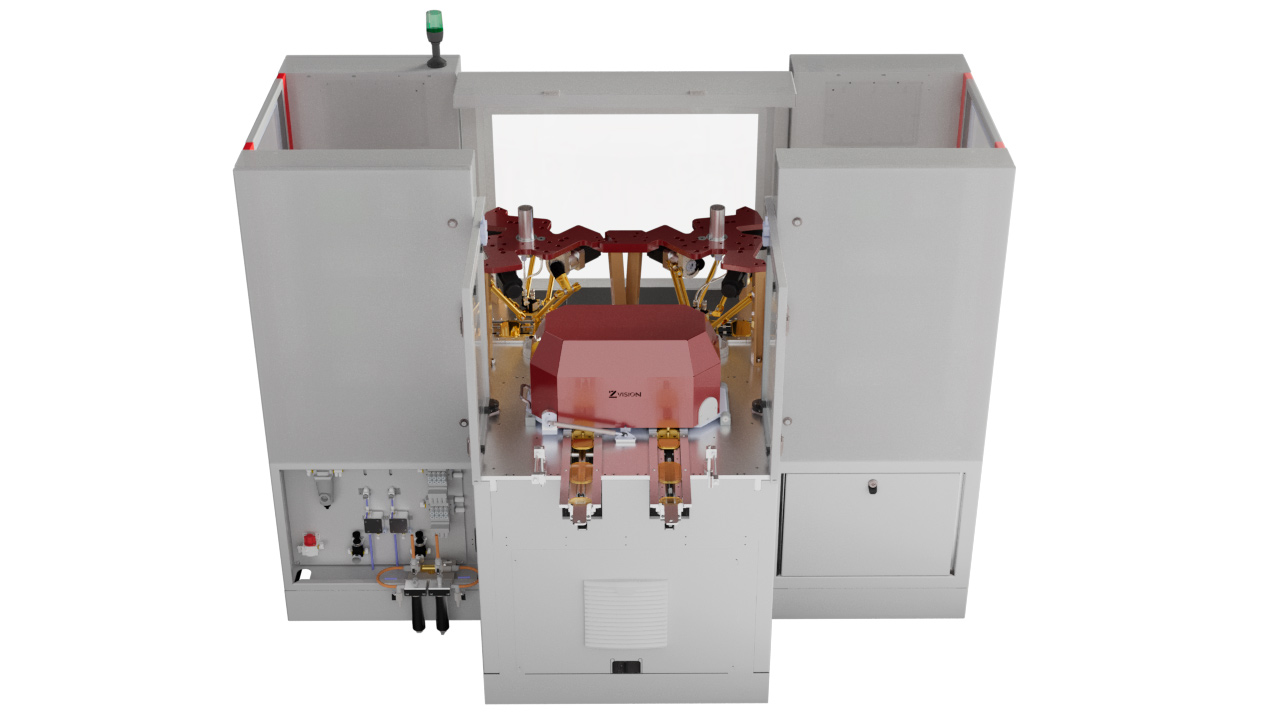
The CDL600 integrates curling and compound lining in a double-lane configuration, based on the high-speed concept of the SL300, but designed to operate simultaneously on two lanes with transverse feeding.
The feeding system is composed of three knives positioner per lane, and ends are introduced in a transverse position (short side leading). This configuration increases pitch density between pieces and improves productivity without requiring additional floor space.
Engineered for maximum production capacity, the CDL600 combines high speed, precision, and reliability in a single machine.
Explore Our Technology in Action
Automatic Cleaning System
The CDL600 incorporates the same automatic cleaning system in each lining head.
The system consists of:
- Cleaning brush
- Purge station
- Water tank with automatic pumping system
At configurable intervals via the touchscreen:
- The head automatically moves to the cleaning station.
- The nozzle passes through the brush to remove external compound residues.
- The compound inside the injector is purged.
- The nozzle passes through the brush again before returning to the working position.
During production stops:
- The nozzle is positioned inside the water tank to prevent air ingress.
- This avoids compound drying inside the injector.
- Before restarting production, the full brush → purge → brush cycle is automatically executed.
This system ensures operational continuity, process stability, and reduced manual intervention.
Curling Station
-
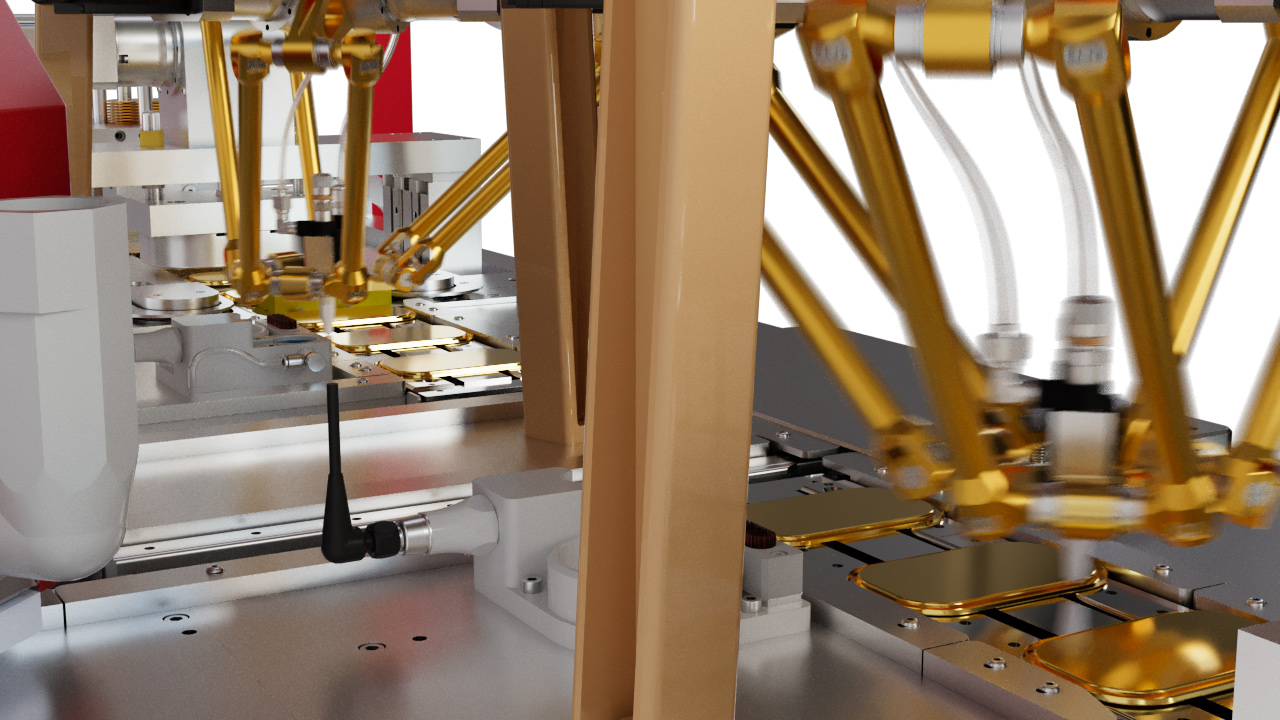
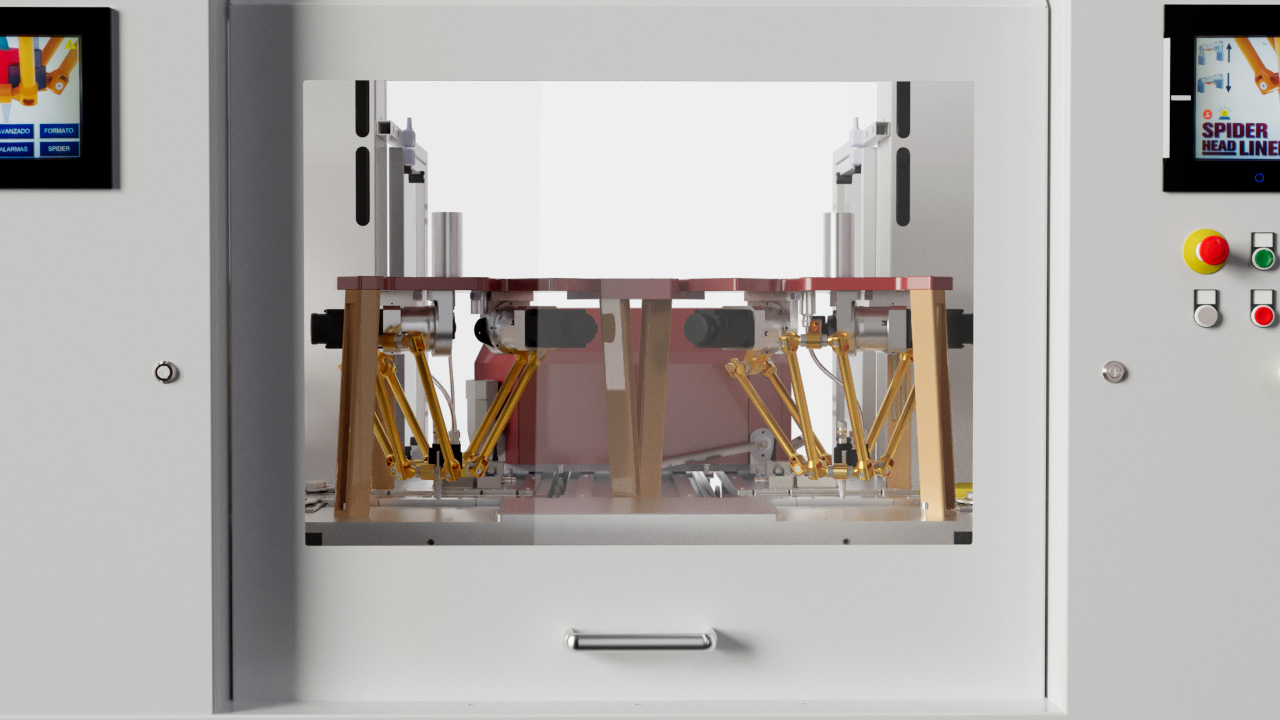
Each lane incorporates a fully servo-controlled curling module.
The curl forming process is performed by a die set driven by two independent servo motors per lane:
- One acting on the upper tooling
- One acting on the lower tooling
The dual-servo system reduces cycle time by approximately half compared to traditional solutions, where the lower tool must complete a longer stroke.
Servo-controlled operation provides:
- High precision during die impact
- Fine adjustment of curl height via the touchscreen interface (degree-based regulation)
- Repeatability in continuous production
End presence detection prevents die collision when no end is present, reducing:
- Operating noise
- Premature tooling wear
- Maintenance requirements
During the curling process, ends are transported by four lateral fingers per lane, driven by two high-precision endless side belts, ensuring stable positioning and accurate handling.
Lining Station
After curling, each end moves to its corresponding lining station.
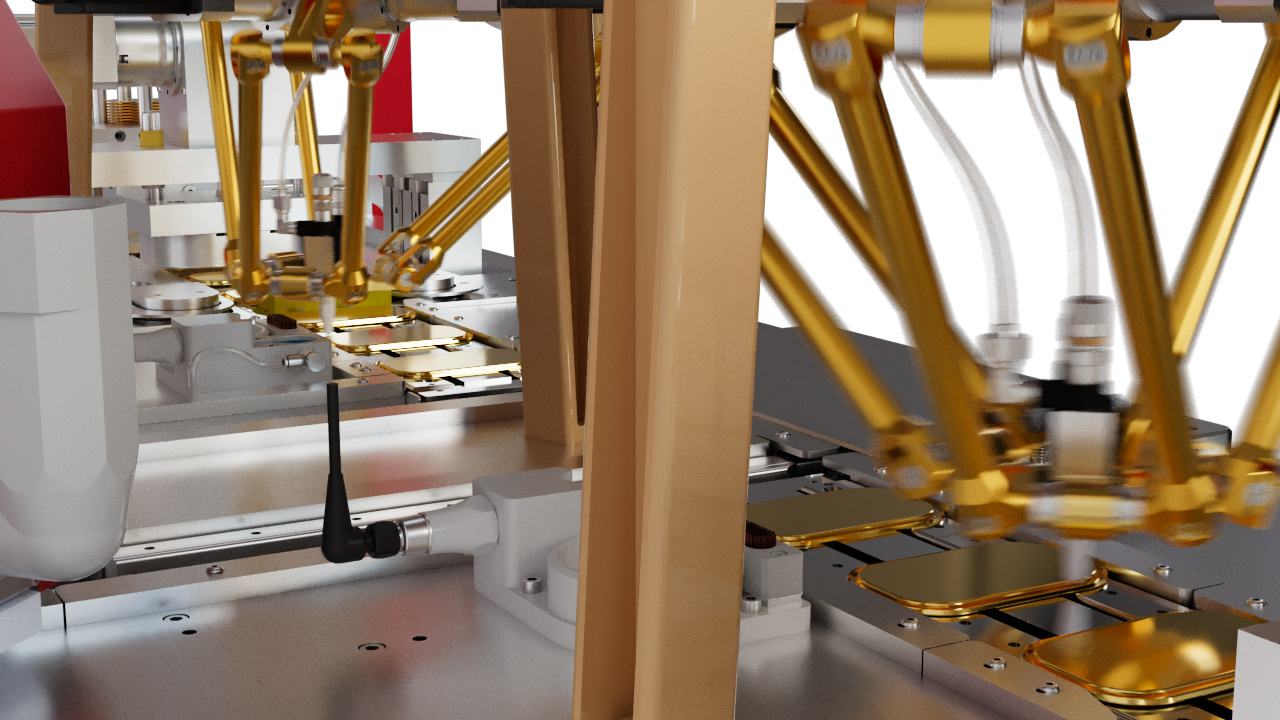
Compound application is performed by the Spider Head Liner heads (one per lane), ensuring:
- Constant linear speed
- Constant pressure
- Uniform and stable compound distribution
The injector follows the movement of each end during application, completing the lining process in a single cycle.
The estimated production capacity is up to 600 ends per minute (depending on format and configuration), distributed across both lanes.
After lining, ends are transferred to a secondary belt positioned at 90°, returning them to their standard orientation for proper entry into the curing oven.
Key Benefits
- Transverse feeding in the entry module
- Double-lane high-speed curling and lining
- Dual-servo die system per lane
- Output up to 600 ends per minute
- Precise curl height adjustment via touchscreen
- Anti-collision protection for tooling
- Single-cycle compound application
- 90° transfer for oven integration
- Automatic cleaning system on both lanes
- Maximum productivity with compact design
- Industrial production-oriented equipment
Image gallery
CDL500
telephone
info@matriruiz.com
address
C/ Aldebarán, 26. Buzón 28 Pol. Ind. La Estrella 30500 Molina de Segura MURCIA. (SPAIN)